✓SMD Flow Control QA Inspection Team
•Published: 2026-05-20•⏱ 8 min read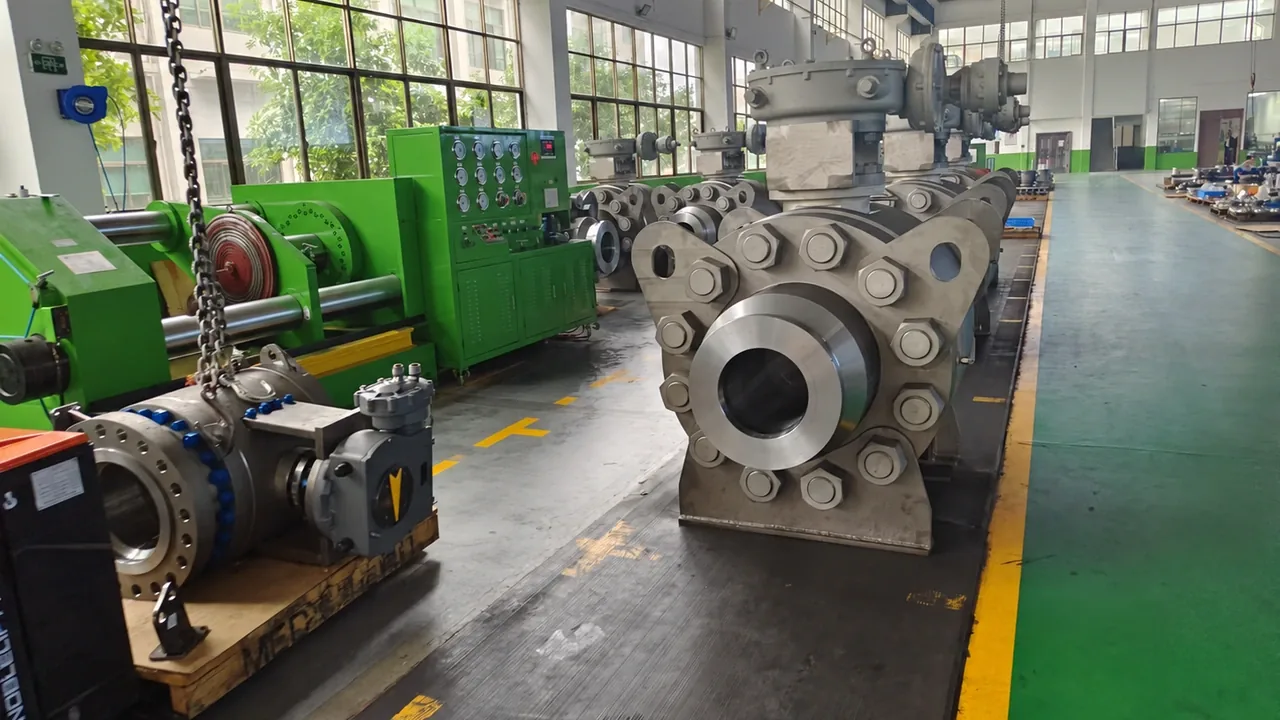
FACTORY EVIDENCE · 100% REAL WORKSHOP
Factory pressure testing is the final quality verification gate ensuring every manufactured industrial valve meets pressure-containment integrity and sealing shutoff criteria before shipment. The two primary international inspection standards governing valve testing are API 598 (Valve Inspection and Testing) and ISO 5208 (Industrial Valves - Pressure Testing of Metallic Valves).
The test sequence begins with the Hydrostatic Shell Test conducted at 1.5 times the valve Cold Working Pressure (CWP) rating at 38°C (100°F). The valve is partially opened, ends are blanked, and test water is pressurized to 1.5x CWP. Holding durations range from 15 seconds for valves ≤ 2" up to 300 seconds for valves ≥ 14". Zero structural deformation, wall sweating, or packing leakage is permitted.
Next, the High-Pressure Hydrostatic Seat Test is performed at 1.1 times CWP with the valve closed, testing each seat independently. For resilient soft-seated valves (PTFE, PEEK, FKM), zero visible leakage is mandatory. For metal-seated valves, API 598 Table 6 defines allowable drop leakage rates (e.g., maximum 20 drops/min for 6" valves). Finally, the Low-Pressure Pneumatic Seat Test is conducted at 80 psig (5.5 bar) using dry air or nitrogen, submerged or bubble-tube monitored.
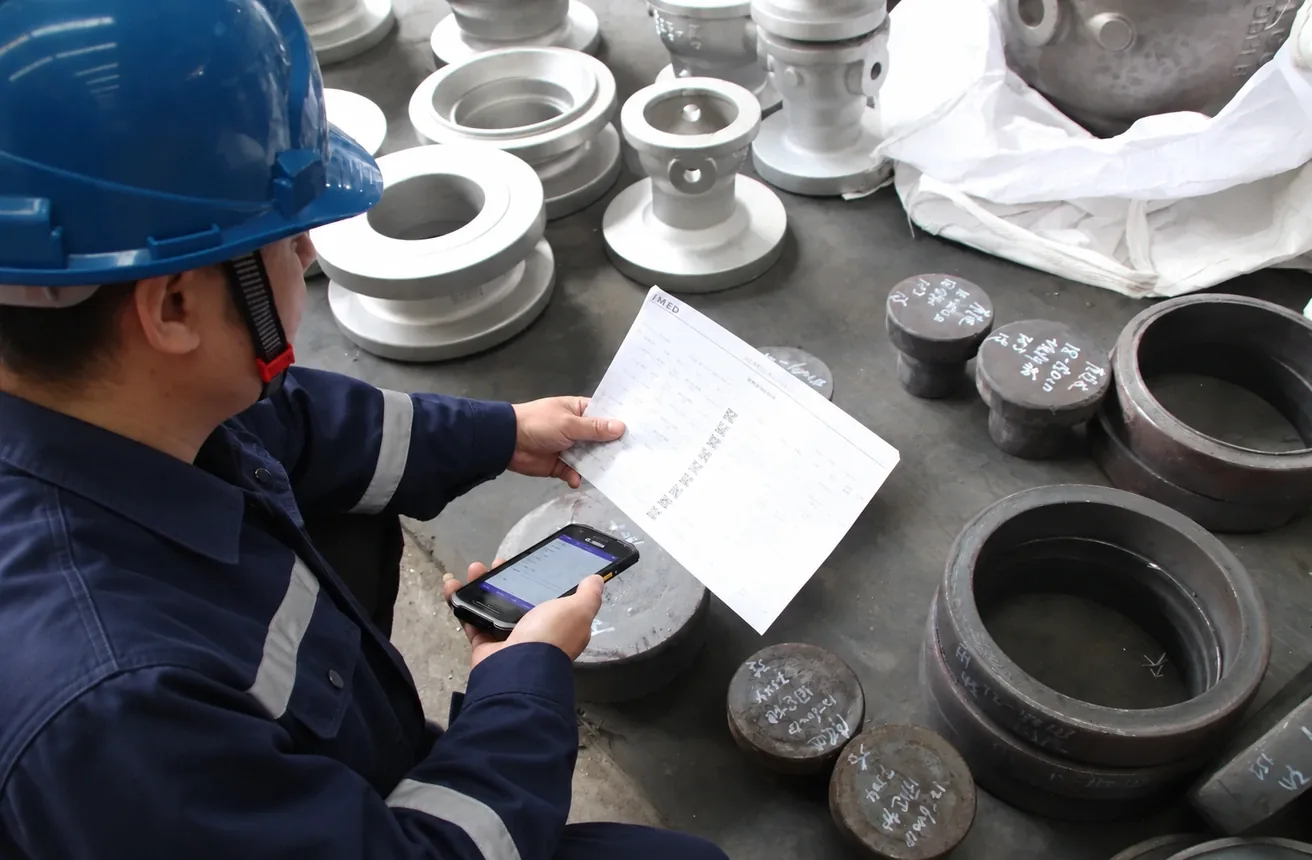
A critical quality requirement for austenitic stainless steel (ASTM A351 CF8M, CF3M) and duplex stainless steel valves is test water chemistry. Chloride ions in test water accelerate stress corrosion cracking (SCC) and pitting in micro-crevices. SMD Flow Control strictly enforces demineralized water with chloride content controlled below 25 ppm (25 mg/L) with rapid hot-air drying and preservation immediately after test completion.
Engineering Q&A
Technical FAQ & Design Criteria
Critical engineering answers referenced against API / ASME / ISO standards.
What is the maximum allowable chloride concentration in test water for stainless steel valves under API 598?↓
For austenitic and duplex stainless steel valves (e.g., CF8M, CF3M, A995 4A/5A), test water chloride content must strictly not exceed 25 ppm (25 mg/L) to prevent chloride-induced pitting and stress corrosion cracking (SCC).
What is the required hydrostatic shell test holding time for a 16" (DN400) Class 600 valve under API 598?↓
Under API 598 Table 4, valves nominal size ≥ 14" (DN350) require a minimum shell test holding duration of 300 seconds (5 minutes) after full test pressure stabilization with zero allowable leakage.
How does ISO 5208 define leakage rate classes compared to API 598?↓
ISO 5208 uses lettered leakage rates: Rate A defines zero detectable leakage (mandatory for soft seats); Rates B, C, and D define specific volumetric leakage allowances in mm³/s based on nominal bore for metal-to-metal seating.
Tags:#API 598#ISO 5208#Pressure Testing#Hydrostatic Test#Chloride Control
Share This Engineering Guide
Pass this technical specification and valve standard breakdown to your project procurement and piping design colleagues.
Factory Pressure Testing Procedures: API 598 vs ISO 5208 Compliance
Official engineering resource by SMD Flow Control